From the Maker’s Bench
Insights from our network of 3d print operators and designers.
You don’t really convert an STL to G-code, you slice it. Open the STL in the slicer made for your printer, choose your printer, nozzle and filament, press Slice, then send the result to the printer or export it to a USB stick or SD card. The file you get only works on the printer you sliced it for, so always slice for your own machine. For Bambu Lab printers, many in our network slice in Bambu Studio and send the job over the network. For most other printers, OrcaSlicer is the favorite choice.
File is a STEP, OBJ or 3MF? Most slicers open those directly. If a tool or service insists on STL, convert it free with our STEP to STL, OBJ to STL or 3MF to STL converter.
About to print a G-code file someone else sliced? Read the G-code safety checklist first.
Use the slicer your printer’s maker ships, because it already has the right printer profile: bed size, nozzle, firmware and the start routine that heats, homes and levels. Five of these are built on OrcaSlicer, so the steps below look almost the same in all of them.
| Your printer | Slicer (October 2026) | Button to press | File you get |
|---|---|---|---|
| Bambu Lab (A1, P1S, P2S, X1, H2D) | Bambu Studio 2.8 | “Print plate” (network) or “Export plate sliced file” (microSD) | .gcode.3mf |
| Prusa (MINI, MK4, XL, CORE One) | PrusaSlicer 2.9 | “Export G-code” or “Export to SD card / Flash drive” | .bgcode (MINI, MK4, XL) or .gcode |
| Creality | Creality Print 7 (Orca-based) | Slice, then print over the network or export (Orca layout) | .gcode |
| ELEGOO | ElegooSlicer 1.5 (Orca-based) | Slice, then print over the network or export (Orca layout) | .gcode |
| Anycubic | Anycubic Slicer Next (Orca-based) | Slice, then print over the network or export (Orca layout) | .gcode |
| Flashforge | Flash Studio (formerly Orca-Flashforge) | Slice, then print over the network or export (Orca layout) | .gcode |
| Klipper, Marlin or anything else | OrcaSlicer 2.4 or UltiMaker Cura 5.13 | “Export G-code file” (Orca) or “Save to Disk” (Cura) | .gcode |
All of these are free. Download them from the printer maker’s website or the slicer’s official GitHub page, never from a download mirror.

The button names below are from Bambu Studio and OrcaSlicer. PrusaSlicer and Cura use the same steps with slightly different labels (see the next section).
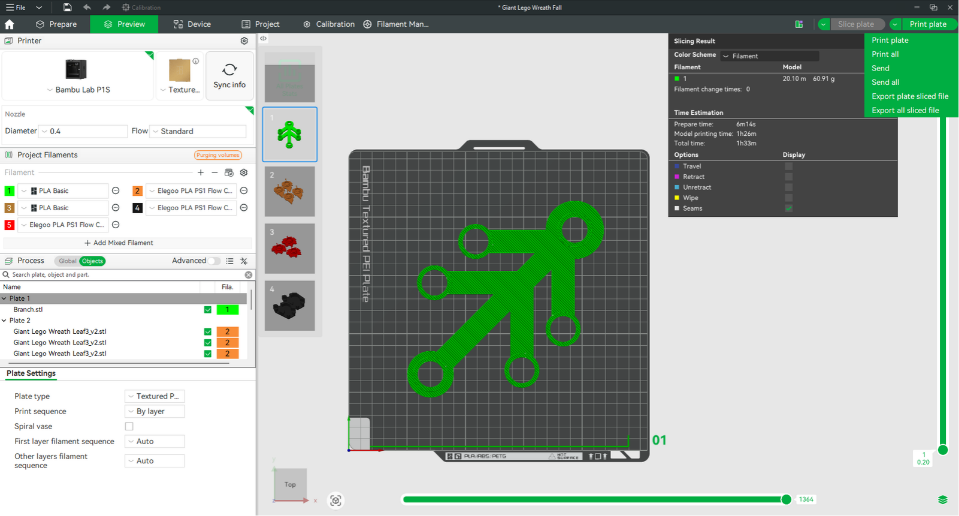
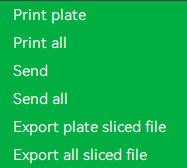
After “Slice plate”, open the arrow next to “Print plate”. With a Bambu printer selected you get “Print plate” and “Send”, which go over the network, and “Export plate sliced file”, which saves a .gcode.3mf for the microSD card. “Export G-code file” (plain .gcode) only appears when a non-Bambu printer is selected. Bambu printers want the .gcode.3mf: it holds the G-code plus the thumbnail and AMS color data. On our Bambu Lab printers we use the Generic PLA profile with our own pressure-advance values, and press “Print plate”. Bambu Studio also warns you when the printer you picked doesn’t match the one you’re sending to.
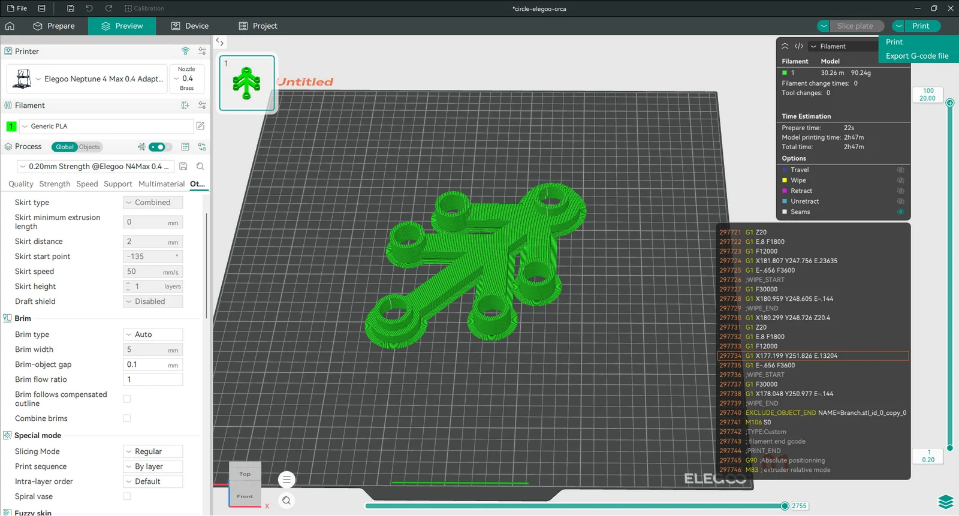
To open an STL in OrcaSlicer, drag it onto the plate or use File → Import (Ctrl+I); OrcaSlicer also opens 3MF, STEP, OBJ and AMF files. Then “Slice plate”, and open the arrow next to the print button: “Print” sends the job to a printer you’ve connected (Klipper/Moonraker, OctoPrint and others) and “Export G-code file” saves it. The vendor versions add their own printers and cloud printing, but the layout is the same. On our Neptune 4 Max we run OrcaSlicer with a heavily customized start G-code and Klipper printer.cfg (adaptive bed mesh, SCREWS_TILT_ADJUST) — which is exactly why G-code from our machine wouldn’t run properly on yours.
Press “Slice now”, then “Export G-code” (Ctrl+G). With a USB stick or SD card plugged in you also get “Export to SD card / Flash drive” (Ctrl+U), and “Send to printer” once a networked printer is set up. Since PrusaSlicer 2.7, Prusa MINI, MK4 and XL printers get binary G-code (.bgcode) by default: about 70% smaller and read by Prusa firmware 5.1 and newer. If you print through OctoPrint, switch it off or use File → Convert.

Add your printer under Settings → Printer → Add printer, open the STL, pick the material and a profile, and press “Slice”. Check the Preview tab, then “Save to Disk” or “Save to Removable Drive”. Cura isn’t Orca-based and has its own settings names, but it works for most Marlin and Klipper printers.
| File | What it is | Who uses it |
|---|---|---|
| .gcode | Plain-text machine instructions for one printer | Most Marlin and Klipper printers (Creality, ELEGOO, Anycubic, Voron and more) |
| .gcode.3mf | G-code packed with a preview image and filament/AMS data | Bambu Lab printers (and OrcaSlicer, if you turn it on) |
| .bgcode | Compressed binary G-code | Prusa MINI, MK4 and XL on firmware 5.1 and newer |
| .3mf (project) | The model plus your slicer settings, not sliced yet | Sharing a print setup; open it in a slicer and slice it for your printer |
| .stl | The shape only: triangles, no units, no settings | What you download and slice |
G-code is a list of moves and temperatures for one specific machine. Run a file made for a different printer and it can drive the nozzle into the bed, move past the end of an axis or heat to the wrong temperature.
Yes, but pick a real slicer, not a generic file converter.
No printer, or no time? Upload the STL (or a 3MF, OBJ, STEP or STP) and get an instant quote. A maker in our network prints it and ships it to you; you never touch G-code.
Model won’t slice, or needs changes? Broken meshes, missing walls and parts that need resizing or splitting go to a designer: start a free engineer chat.
Already slicing like a pro? Print orders for others on Intagly.
| Mistake | What you see | Fix |
|---|---|---|
| Wrong printer or nozzle profile | Nozzle scrapes or crashes, print in the wrong spot, warning on the printer | Select your exact printer and fitted nozzle, then re-slice |
| Wrong filament profile | Stringing, poor layer bonding, clogs | Pick the profile for the spool you loaded (PLA, PETG, TPU…) |
| Model designed in inches | Model imports tiny | Scale by 2540%, or use our STL scaler |
| No supports | Overhangs droop, parts start in mid-air | Turn on supports (tree supports leave fewer marks) |
| Model not flat on the bed | Only a corner touches the plate | Use “Lay on face” and re-slice |
| First layer too high or too low | Print won’t stick, or the first layer is see-through or rough | Re-run bed leveling; clean the plate; adjust Z offset |
| Wrong file type for the printer | Printer doesn’t list the file | Bambu: .gcode.3mf. Prusa MINI/MK4/XL: .bgcode. Others: .gcode |
Start with PLA: it prints at low temperatures, needs no enclosure, and every slicer’s Generic PLA profile works with it out of the box. These are the spools we buy again and again. Move to PETG when a part has to take heat or a knock (see our PETG filament guide). Skip carbon-fiber and other specialty filaments for a first print: they need a hardened nozzle and tuned settings. For most prints, filament is the biggest cost per part, so our makers stock up on these spools when they’re discounted. Check the current price before you buy.
| Use | Spool | Slicer profile | |
|---|---|---|---|
| First prints (what we use most) | ELEGOO PLA | Generic PLA | Check price |
| First prints, fast printers | OVERTURE PLA | Generic PLA | Check price |
| Tougher, heat-resistant parts | OVERTURE PETG | Generic PETG | Check price |
Still choosing a printer? Our best 3D printers under $300 guide compares the ones we’d buy.
An STL describes a shape as thousands of triangles. It has no units, no colors and no print settings. G-code is the opposite: a plain-text list of instructions for one printer — heat to this temperature, move here, push out this much plastic. A short print has thousands of lines. Here are a few, explained:
| G-code line | What it tells the printer |
|---|---|
| M140 S60 | Heat the bed to 60 °C (and keep going) |
| M104 S210 | Heat the nozzle to 210 °C |
| G28 | Home all axes |
| G1 X50 Y50 Z0.2 F3000 | Move to X50 Y50, 0.2 mm above the bed, at 3,000 mm per minute |
| G1 X100 Y50 E5 F1500 | Move 50 mm along X while pushing out 5 mm of filament |
OrcaSlicer shows the real file next to the preview: in the screenshot above, the panel on the right lists the last lines of a Neptune 4 Max job, including the Klipper-only EXCLUDE_OBJECT_END line — another reason G-code doesn’t move between printers.
A 3MF sits in between: it can hold the shape plus your slicer settings, but it still has to be sliced. For the full comparison of STL, OBJ, 3MF, STEP and G-code, see our 3D printing file types guide.
Open the STL in a slicer (Bambu Studio, OrcaSlicer, PrusaSlicer or Cura), select your printer, nozzle and filament, press Slice, then send or export the file. See the step-by-step above.
Yes. Kiri:Moto slices in your browser and Prusa EasyPrint slices on Prusa’s servers, both free. A desktop slicer is still the safer choice, because it carries your printer’s exact profile.
Yes, with a cloud slicer app such as Prusa EasyPrint (Prusa app) or Creality Cloud. Bambu Handy reprints MakerWorld models but isn’t made for slicing your own STL.
Drag it onto the build plate, or use File → Import (Ctrl+I). Then press “Slice plate”, and “Print” or “Export G-code file”.
Open the STL, choose your printer and material, press “Slice”, then “Save to Disk” or “Save to Removable Drive”.
Yes, packed inside a .gcode.3mf file. Bambu Studio sends it over the network with “Print plate”, or saves it for the microSD card with “Export plate sliced file”.
An STL is the shape of the object. G-code is the set of instructions that tells one particular printer how to build that shape, layer by layer.
Only roughly. Tools can turn the toolpaths back into a mesh, but infill, supports and seams are baked in and the original surfaces are gone. Ask the designer for the STL or 3MF instead.
Usually the file type is wrong (Bambu wants .gcode.3mf, recent Prusas default to .bgcode), the file was sliced for another printer, or the file name or card format isn’t one the printer accepts. Re-slice for your printer and export again.
*Some links in this guide are Amazon affiliate links. As an Amazon Associate, Intagly earns from qualifying purchases, at no extra cost to you.